
AMD EPYC SP6 CPU cooling
AMD SP6 CPU Liquid Cold Plate
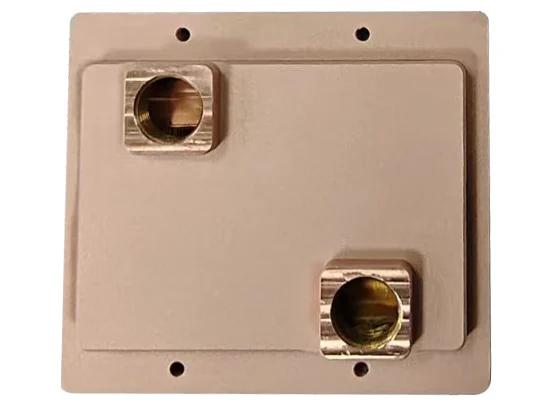
Copper liquid cold plate for AMD EPYC SP6-socket server CPUs: 300 W heat load on a TLP diffusion-bonded plate in a 120 × 79 × 16 mm envelope, CFD validated before tooling and leak tested in production.
Request a quote
Download datasheet (PDF)
Key specifications
| Model | T-HS202319 — AMD SP6 CPU liquid cold plate |
|---|---|
| Heat dissipation | 300 W |
| Material | Copper (red copper), CNC machined |
| Joining method | Transient liquid-phase (TLP) diffusion bonding |
| Test conditions | 40% EGW coolant, 40°C inlet temperature |
| Flow rate / pressure drop | 3.3 LPM at 3 kPa |
| Cold plate surface temperature | ≤55°C under rated load |
| Working pressure | 1 MPa |
| Dimensions | 120 × 79 × 16 mm |
| Thermal resistance (plate, rated point) | ≤0.050 °C/W — calculated as (surface-temperature limit − coolant inlet) / heat load: (55 − 40)°C / 300 W |
| ΔP–flow curve | Measured ΔP–flow curve is supplied with the prototype test report and DFM review — request it with your drawing |
| Wetted materials | Copper (C1100 / T2) channel and port surfaces; fittings, tubing and quick disconnects per customer specification — confirmed against your coolant during DFM |
| CAD / drawings | STEP model and 2D drawing available under NDA — request with your RFQ |
| Validation | CFD flow and thermal simulation; helium leak and proof-pressure testing |
AMD SP6 CPU Liquid Cold Plate datasheet (PDF)
Full specification table, dimensions, coolant and test conditions, materials and joining method — ready to drop into your thermal review.
ToneCooling manufactures the AMD SP6 CPU Liquid Cold Plate — 300 W, CFD-validated before tooling and 100% leak tested under ISO 9001 at our Guangdong technical center, with North American customers supported by ToneCooling Texas LLC.
Why ToneCooling
Design, engineering, and manufacturing run in-house at the ToneCooling technical center in Guangdong — one accountable partner from CFD model to leak-tested hardware. Transient liquid-phase gives the assembly durable joints under repeated thermal cycling, and every part ships with the test documentation your qualification process needs. Prototype orders start from 1 piece with a 4–6 week prototype lead time, so an evaluation unit reaches your lab fast.
Routine production testing
Acceptance criteria are agreed in writing before quotation, and the inspection results ship with the parts:
Leak testing (100% of units) — helium leak test to ≤1×10⁻⁹ mbar·L/s or nitrogen pressure-decay, per the agreed criteria.
Proof-pressure testing — to the project requirement, with burst verification on qualification samples.
Flow-resistance check — verified against the rated pressure-drop window at the specified flow rate.
Dimensional and flatness inspection — at the TIM interface, to drawing tolerances.
Bond inspection — diffusion-bonded parts are ultrasonically C-scanned per ASTM E2375; thermal-cycling qualification per IEC 60068-2-14 on qualification samples.
CFD validation before tooling
Before any metal is cut, the design is simulated against your operating point. The CFD model answers the questions that decide whether the plate survives qualification:
Channel layout — the flow path is placed over the die hot spots so the coldest coolant reaches the highest heat flux first.
Pressure drop — the channel network is tuned so the plate stays inside your pump budget at the rated 3.3 LPM flow.
Surface temperature — predicted case temperatures are checked against the ≤55°C limit before the design is frozen.
The simulation report ships with the DFM review, and the prototype is then verified on the bench: measured ΔP–flow curve and thermal resistance against the CFD prediction, plus helium leak and proof-pressure testing.
Applications
AMD EPYC SP6 telco, edge and energy-efficient server platforms on direct-to-chip liquid cooling — compact sockets and tight power budgets that still benefit from liquid-cooled density.
Engineering Support Pages for CPU Cold Plate RFQs
Use these pages to prepare socket drawings, heat load, coolant, flow rate, pressure-drop target, port layout, validation scope and module envelope before quotation.
 Server CPU Cold Plate RFQ ChecklistUse for SP6 drawing, heat load, coolant, flow and pressure-drop inputs.
 Pressure Drop and Flow Rate ReviewPrepare flow rate, coolant, inlet temperature and pump pressure budget.
 Port Layout and Hose RoutingReview fitting direction, hose clearance, bend radius and service access.
 Leak, Pressure and Cleanliness ValidationDefine leak test, pressure test, cleanliness and documentation scope.
 Server Module Envelope Review1U, 2U and custom chassis envelope, tube route and service access.
AMD SP6 CPU Liquid Cold Plate FAQ
Which CPUs does this plate fit?
AMD EPYC SP6-socket processors at up to 300 W. Mounting and port locations follow your platform drawing.
Why does the SP6 plate specify 3.3 LPM?
That flow holds the surface at or below 55°C at 300 W with 40% EGW — keeping the temperature rise small on loops that run warm. Lower-flow operating points are validated by CFD during DFM.
Is this plate suited to telco and edge enclosures?
Yes — SP6 targets dense, power-efficient platforms, and the 120 × 79 × 16 mm plate fits short-depth chassis where fan noise and airflow are the binding constraints.
What coolant should be used?
Rated performance is tested with 40% EGW at 40°C inlet. Data-center loops following ASHRAE W55 water quality are supported; alternative mixtures are reviewed during DFM.
What flow rate does it need?
3.3 LPM at 3 kPa under rated load. Your pump budget and manifold layout are checked against this during engineering review.
Can the design be customized?
Yes. Port locations, hose routing, mounting pattern, and surface finish are customized from your drawings. CFD simulation validates the change before tooling.
What is the Quantity and lead time?
Prototype orders start from 1 piece with a 4–6 weeks lead time from approved drawing and PO; production runs 6–8 weeks.
How is quality verified before shipment?
Helium leak testing and proof-pressure testing on the production line, plus flatness and dimensional checks to the acceptance criteria agreed in writing before quotation.
Request a quote
Send your drawing, heat map, coolant, and flow budget to info@tonecooling.com or use the quote form — the engineering team returns a manufacturable concept with the quotation. prototypes from 1 piece, prototype in 4–6 weeks.
Send drawings for engineering review or download the datasheet (PDF)

